Can photomask inspection equipment detect smaller defects?
Author
Date Published
Reading Time
Photomask inspection equipment can detect increasingly small defects, but practical sensitivity depends on the inspection method, mask design, defect type, and operating conditions. A minimum detectable defect specification is only a starting point: detection probability, nuisance rates, throughput, and validation on representative masks also matter. The question for a technical evaluation is not simply how small a defect the tool can see, but whether it can find the defects that matter on the masks it will inspect, often enough and fast enough for the intended workflow.
A smaller number does not tell the whole story
A supplier may quote a minimum detectable defect size, but that number has little value without the conditions behind it. Was the defect an opaque particle, a clear intrusion into an absorber line, a line extension, or a subtle pattern variation? Was it isolated in an open area or embedded in dense features? Was it detected once, or repeatedly with a stated probability?
Defect dimensions also need a common reference. A dimension measured on the mask is not automatically the same as its projected dimension on the wafer; the relationship depends on the lithography system’s reduction ratio. Comparing a mask-plane specification from one supplier with a wafer-plane figure from another can make an ordinary performance difference look dramatic.
Even when size is defined consistently, printability remains a separate question. A small defect in a sensitive pattern location may influence the wafer image, while a larger feature elsewhere may have no meaningful effect under the intended exposure conditions. Inspection should therefore be evaluated against defect types and process risks, not against size alone.
What the inspection system is actually comparing
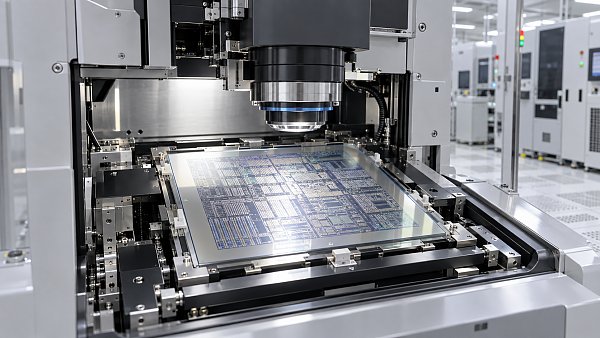
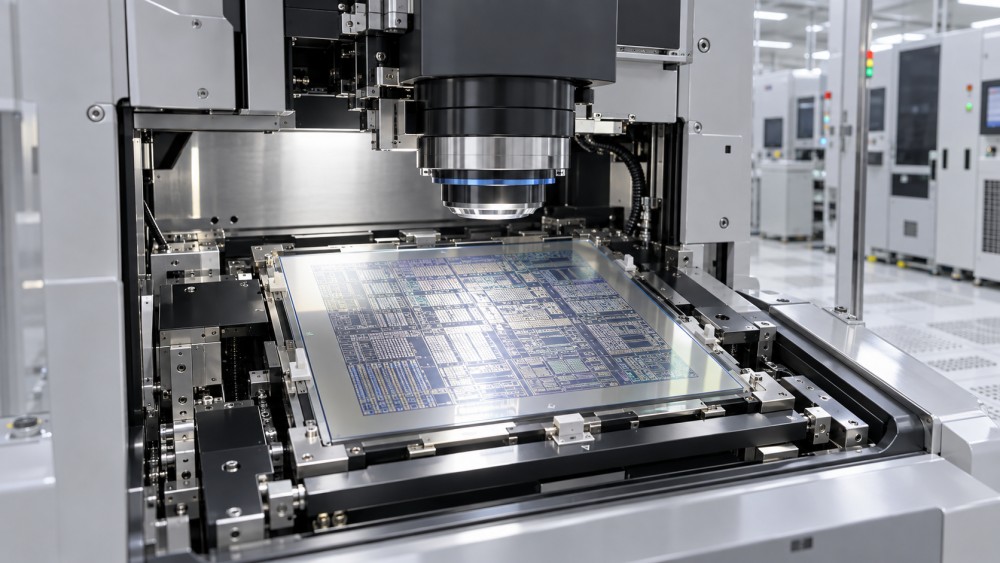
Most patterned-mask inspection approaches look for differences between an acquired image and a reference. In die-to-die inspection, corresponding repeated areas are compared with each other. This can work well when the mask contains suitable repetitions, but a systematic defect repeated in every compared die may not stand out as a difference. The method also depends on accurate alignment and appropriate handling of legitimate variation.
Die-to-database inspection compares the measured pattern with a reference derived from design data. It is useful when there is no suitable repeated structure, but its performance depends on how well the reference represents the intended manufactured image. Complex features, proximity corrections, and expected process variation can make reference generation and threshold setting consequential parts of the evaluation.
Shorter-wavelength optical inspection can improve sensitivity to fine features, but wavelength alone does not establish performance. Illumination, collection optics, image processing, noise, mask materials, and inspection recipe all affect the usable result. Electron-beam approaches offer another path to fine-feature inspection, with different throughput and operational trade-offs. A tool that resolves a feature in a demonstration is not necessarily the best choice for routine inspection of a full mask set.
Extreme ultraviolet masks deserve separate treatment. They are reflective masks with a multilayer structure, so the relevant defect population can include issues associated with the multilayer as well as the patterned absorber and contamination. Actinic inspection uses EUV-wavelength illumination to assess the mask under optically relevant conditions. Other inspection methods may still be useful, but their signals and detection limits should not be assumed to match actinic behavior.
Sensitivity is a probability, not a guaranteed cutoff
In practice, detection does not switch abruptly from impossible to certain at one defect size. A useful evaluation asks for a probability-of-detection curve, or equivalent evidence, across relevant defect sizes and types. The curve should identify the mask pattern, defect construction, inspection recipe, sample population, and decision threshold. Confidence in the result depends on how many representative examples were tested; a handful of detections does not establish a robust probability.
Request results separately for the defect classes that matter. A tool may perform differently on isolated particles, edge deviations, pinholes, and low-contrast pattern changes, even when their nominal dimensions are similar. Orientation and location can matter too: a defect at a line edge may produce a different signal from one in an open field.
Then examine what happens when sensitivity is increased. More aggressive thresholds can capture weaker signals, but they can also generate more nuisance detections: flagged locations that are not actionable defects. Those calls consume review time and can obscure the truly critical findings. A supplier’s best sensitivity result should be paired with its nuisance rate at the same settings, not with a throughput figure measured using a less demanding recipe.
Review capacity can become the bottleneck
Consider a mask shop evaluating a more sensitive recipe for a dense critical layer. The recipe may find additional candidates, but if the review station cannot classify them before the next production milestone, the practical benefit is limited. The decision may be to use that recipe only on selected masks or regions, while retaining a faster inspection for lower-risk work.
This is a workflow choice, not a reason to dismiss sensitivity. Ask how candidate locations are transferred to review, whether coordinates remain accurate across tools, and how classifications feed back into recipe tuning. If defect disposition depends on wafer impact, establish who will perform that assessment and what evidence is required before release or repair.
Build the comparison around representative masks
A demonstration on a convenient test plate can screen suppliers, but it should not be the final acceptance test. Use masks or test structures that represent the intended pattern density, feature geometries, materials, and inspection regions. Include the difficult cases: dense arrays, isolated features, transitions between pattern types, and areas where the current process produces nuisance calls.
Where possible, include defects with independently characterized locations and dimensions, along with naturally occurring defects from the relevant process. Programmed defects can provide controlled comparisons, but they may not reproduce the shapes, contrast, or surface conditions of production defects. The characterization method has its own uncertainty, so record how each reference defect was measured and avoid treating every assigned dimension as exact.
A blind or partially blind test can make the comparison more credible: the evaluator retains the reference locations while the supplier runs an agreed recipe. The protocol should also state whether recipe tuning is allowed, how much time is available, and whether results from repeat scans can be combined. Otherwise, one tool may receive substantially more preparation than another.
The following evidence is worth requesting before a purchase decision:
- Detection performance: results by defect type, size, pattern context, and probability, with sample counts and uncertainty or confidence limits where available.
- False and nuisance calls: counts or rates with a clear denominator, inspection area, classification method, and the same recipe used for sensitivity testing.
- Repeatability: repeated scans showing both missed detections and variation in reported locations under defined operating conditions.
- Coverage: supported mask types, dimensions, patterned areas, exclusions, and any restrictions involving pellicles or handling.
- Production timing: scan time, setup, loading, recipe changes, data transfer, and downstream review time for the proposed mask mix.
Separate vendor-demonstrated capability from a qualified production process. If the relevant mask material, pattern, or defect class has not yet been tested, record it as an open qualification item rather than assuming that a neighboring result applies.
Throughput and cost depend on the recipe
Inspection throughput is often presented as a maximum, but the production question is different: how many masks can be cleared under the required sensitivity, coverage, and review rules? Fine sampling, complex reference generation, rescans, and high candidate counts can change turnaround time. Loading and unloading, calibration, planned maintenance, and interruptions also affect available capacity.
Compare suppliers on an agreed workload rather than a headline masks-per-hour figure. Define the mask mix, inspected area, recipe settings, operating schedule, and treatment of review. A high-volume mask shop may value a balanced recipe and dependable uptime; a development line may accept slower inspection to investigate an unfamiliar defect mechanism. Neither choice is universally better.
Include the less visible obligations in the cost model: installation requirements, clean handling, software and reference-data preparation, operator training, service visits, spare parts, and the time needed to qualify new recipes. If mask data must move across sites or organizational boundaries, confirm data-format compatibility and security arrangements early. A tool can meet its optical specification and still create an integration problem.
Acceptance should cover the system that will be operated
Before signing, translate the evaluation into measurable acceptance conditions. Specify the test masks, defect classes, recipes, detection and nuisance criteria, timing, and repeatability requirements. State where the test will occur, who supplies and maintains the reference samples, and how disagreements about defect classification will be resolved. Protect confidential design data while ensuring that both parties can audit the result.
Service readiness matters as much as the initial demonstration. Check local support coverage, escalation paths, lead times for critical components, software-update policies, and access to applications engineers who can help maintain recipes as mask designs change. A local sales presence alone does not establish that repair capability or replacement parts are available locally.
The strongest choice is not necessarily the instrument with the smallest advertised defect. It is the system that demonstrates adequate detection on the relevant masks, at a nuisance rate and turnaround time the operation can absorb, with a clear route from installation to qualified use. If that evidence is missing, the next step is a defined joint test—not a stronger interpretation of the brochure.
Questions about market trends? Contact Market Scope Live for deeper business insights.
We respect your privacy. Your information is strictly confidential.
We respect your privacy. Your information is strictly confidential.
Related News
 Performance BenchmarksHow does downtime affect semiconductor equipment throughput?Discover how downtime affects semiconductor manufacturing equipment throughput, from lost wafer capacity to recovery delays, and learn practical ways to improve qualified output.MORE+
 Performance BenchmarksHow Should You Compare CMP Equipment Uptime Claims?How should I compare CMP equipment uptime claims? Learn to uncover exclusions, normalize availability data, and assess service support before you buy.MORE+
 Performance BenchmarksCan photomask inspection equipment detect smaller defects?Photomask Inspection Equipment can detect smaller defects—but how reliably? Explore sensitivity, throughput, and key tests to make a confident purchase.MORE+