How to evaluate photomask manufacturers for defect control
Author
Date Published
Reading Time
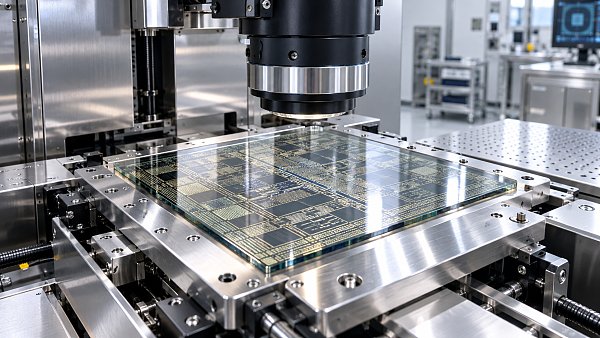
Defects in a photomask can affect lithography yield, making supplier evaluation a critical part of semiconductor process control. When comparing photomask manufacturers, technical teams need more than a headline defect specification: inspection sensitivity, defect classification, repair capability, contamination control, and qualification evidence all matter. The practical question is not simply whether a supplier can find a small defect, but whether it can identify defects that matter to your process and deliver acceptable masks consistently.
A useful evaluation starts with the mask’s intended use. A critical patterned layer for leading-edge lithography, a less demanding process layer, and a mask used for advanced packaging may all require different inspection strategies and acceptance limits. Applying the tightest available specification to every mask can add cost and cycle time without addressing the risks that dominate a particular application.
Define the defect risk before comparing specifications
Give suppliers enough process context to propose a meaningful control plan: mask type, lithography wavelength, pattern characteristics, intended layer, imaging conditions, and the features most sensitive to variation. Include the expected inspection coverage and any restrictions on repair, cleaning, or pellicle use. Confidentiality agreements may be needed before sharing layout and process details.
Separate a defect’s physical appearance from its potential wafer impact. An opaque or clear defect, a local pattern deviation, and a particle may demand different responses. Their significance depends on location, feature geometry, imaging conditions, and whether the effect is printable on the wafer. A defect in a noncritical area may be acceptable under an agreed disposition rule; a smaller anomaly in a sensitive feature may warrant investigation.
This is where comparison often goes wrong. Two suppliers can quote the same nominal defect size while using different detection methods, reference patterns, coverage rules, or definitions of a reportable defect. Ask for the full specification and its conditions, not just the number on a quotation. Make sure the proposed limit applies to the actual mask type and pattern, rather than a generic demonstration sample.
Test what inspection can detect—and what it can miss
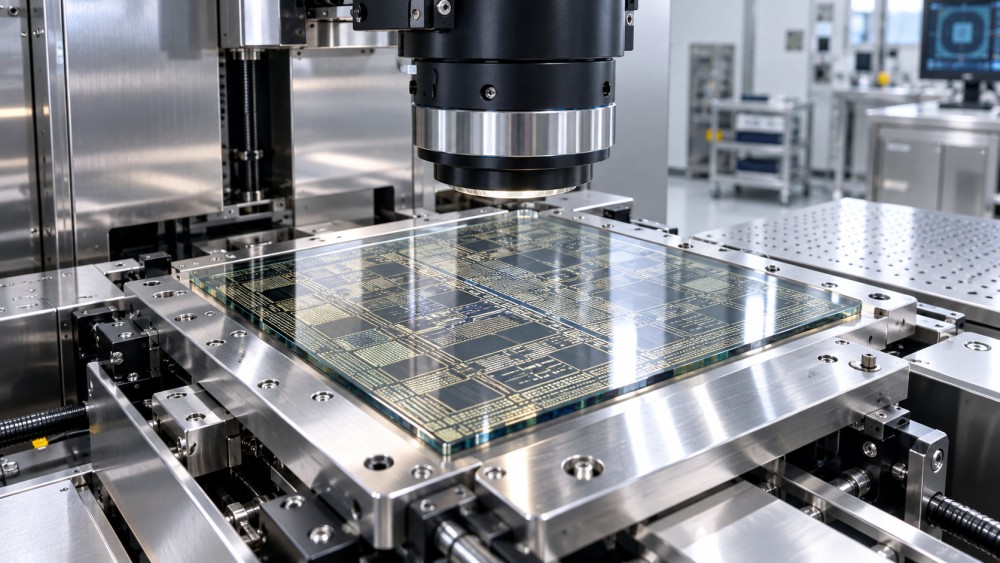
Inspection sensitivity is not a single value that applies equally to every defect. Contrast, pattern density, location, and the inspection recipe can change detectability. A supplier’s ability to detect an isolated programmed defect under controlled conditions is useful evidence, but it does not by itself establish performance across a complex production mask.
Ask which inspection methods are used at each stage, what reference is used for comparison, and how the team handles areas that are difficult to inspect. Die-to-die comparison can be effective where repeated patterns are available; die-to-database methods compare the mask with design data, but require careful alignment and management of design-to-mask differences. Neither method removes the need to understand its limitations for the specific layout.
The review process matters as much as the initial scan. A highly sensitive recipe may generate a large number of nuisance detections, consuming review capacity and extending delivery time. Ask how detections are classified, which require human review, and how uncertain cases are escalated. If a defect is waived, the record should show who authorized it, the reason, and the applicable acceptance rule.
Request evidence of detection performance using relevant test structures or representative masks, including the defect types, sizes, locations, sample boundaries, and inspection settings. Where possible, have the supplier demonstrate repeatability across runs. A clean inspection report is not proof that every relevant defect was detectable.
Follow a defect through review, repair, and release
A supplier’s defect-control capability is best judged as a chain. Inspection finds a candidate; review characterizes it; the team decides whether to accept, repair, or reject the mask; and post-repair verification determines whether the result is suitable for release. A weakness at any handoff can make a strong inspection tool less valuable.
Repair is not automatically the lowest-risk option. Removing unwanted material or adding missing material may leave a residual feature or alter local optical behavior. For a critical pattern, ask how the supplier assesses repair feasibility, what post-repair inspection and metrology are performed, and when a mask is rejected rather than repaired. Depending on the application, wafer-printability assessment or simulation may be needed; agree on who supplies the imaging conditions and who approves the result.
A practical audit question is: “Show us the record for a representative defect from detection to disposition.” The record should connect inspection images, classification, repair history if applicable, verification results, and final approval. Proprietary customer information can be removed. The point is to see whether decisions are traceable, not to obtain another customer’s data.
Look beyond the pattern to contamination control
A mask that leaves pattern fabrication in good condition can still acquire particles or other contamination during cleaning, pellicle mounting, packaging, transport, or subsequent handling. Evaluate the interfaces between these steps, especially when different facilities or subcontractors are involved.
Review how the supplier controls cleaning chemistry, handling equipment, storage containers, and environmental conditions. Ask where inspections occur relative to cleaning and pellicle installation, and how the supplier distinguishes a pattern defect from removable contamination. Cleaning itself can introduce risk, so the relevant question is not how aggressively the mask can be cleaned, but how cleanliness is achieved without compromising the pattern or optical performance.
If a pellicle is part of the flow, confirm the inspection approach for the mask and pellicle, the handling controls, and the procedure for damage or contamination discovered after mounting. For EUV masks, the evaluation needs additional attention to the reflective mask structure and application-specific inspection and pellicle arrangements. Do not assume that a supplier’s established optical-mask flow transfers unchanged to EUV.
Agree on packaging, transport conditions, incoming inspection, and the point at which responsibility transfers. If contamination is found at the fab, a retained inspection record and clear chain of custody make root-cause analysis far more productive than a dispute over whether the mask was clean at shipment.
Qualify the production flow, not just a demonstration mask
A successful sample establishes a starting point. It does not necessarily show that the same result can be repeated across operators, tools, material lots, repairs, and normal production scheduling. Qualification should use representative patterns and agreed acceptance criteria, then examine variation across an appropriate set of masks and production runs. The number and mix of samples should reflect the application’s risk and the evidence already available.
Define what will be measured before the trial begins. Alongside defect disposition, consider relevant pattern fidelity, registration, critical-dimension performance, and other mask requirements for the layer. Establish how results will be compared with the receiving fab’s measurements, including measurement uncertainty and the process for resolving disagreements.
Wafer results can provide important confirmation, but they require careful attribution. A printing problem may involve the mask, resist, exposure conditions, or downstream processing. Agree in advance on the test conditions, reference measurements, and criteria for initiating a joint investigation. Avoid turning a single wafer observation into a supplier-wide performance claim.
Also examine change control. A new inspection recipe, mask blank source, repair process, software version, or production site may alter the qualified flow. Specify which changes require notification, supporting data, customer approval, or requalification. The same discipline applies if the supplier outsources a step after qualification.
Compare capacity and supply risk with the same care
A technically capable supplier may still be a poor fit if critical inspection or repair capacity is constrained when your masks are needed. Ask for standard and expedited lead times, where bottlenecks tend to occur, and how the supplier handles tool downtime or a failed final inspection. Distinguish a quoted turnaround target from demonstrated performance for comparable mask complexity.
Check dependencies on mask blanks, pellicles, specialized materials, and external service providers. A local production site does not necessarily mean a local or diversified supply chain. If continuity is essential, establish what backup capacity exists and whether an alternate facility is already qualified for your mask type. Moving work to another site should not be treated as a routine administrative change if the process has not been validated there.
Price comparisons should include inspection coverage, repair attempts, remake conditions, expedited service, shipping, and the customer’s qualification effort. A lower mask quote may leave the fab carrying more incoming inspection or investigation work. Conversely, paying for inspection capability that has no clear connection to the layer’s risk may not improve the decision.
Put the decision into an evidence-based request
Send shortlisted photomask manufacturers the same application brief and ask them to identify exceptions rather than simply accept a generic specification. A useful response should make the following points clear:
- Which defect classes and mask areas are covered, and under what inspection conditions?
- What evidence supports detection capability on patterns representative of the intended application?
- How are ambiguous defects, repairs, waivers, and post-repair verification documented?
- Which process steps and materials are controlled in-house, and which depend on outside parties?
- What production data, capacity assumptions, and change-notification terms support the proposed delivery plan?
Keep laboratory demonstrations, qualification results, and sustained production records in separate categories when reviewing the answers. That distinction is central to the supply-chain perspective FabBrief plans to bring to semiconductor manufacturing: an announced capability is not the same as a qualified, repeatable service.
Before awarding the work, resolve the open items in the acceptance plan with lithography, mask engineering, quality, and procurement. If a supplier cannot explain how a consequential defect would be detected, dispositioned, and traced through delivery, the remaining risk belongs in the decision—not in a footnote after the purchase order.
Questions about market trends? Contact Market Scope Live for deeper business insights.
We respect your privacy. Your information is strictly confidential.
We respect your privacy. Your information is strictly confidential.
Related News
 Supplier AssessmentHow to evaluate photomask manufacturers for defect controlCompare photomask manufacturers for defect control. Learn what to ask about inspection, repair, contamination and qualification before choosing a supplier.MORE+
 Supplier AssessmentHow to Compare Service Response Times in Equipment ContractsHow do I compare service response times in equipment contracts? Learn how to assess SLAs, coverage, engineer arrival and spare parts to choose the right supplier.MORE+
 Supplier AssessmentHow to Check Software Support for a Used TesterHow do I check tester software support before buying used equipment? Verify licenses, compatibility, updates, and support terms before you commit.MORE+