How temperature uniformity affects diffusion furnace yield
Author
Date Published
Reading Time
Temperature nonuniformity can reduce diffusion furnace yield by producing different dopant profiles across a wafer or from one wafer to another. A small thermal difference may be enough to shift sheet resistance or junction depth toward a process limit, even when the furnace controller reports that every zone is at its setpoint. The manufacturing consequence depends on the recipe, the device’s electrical margins, and the measurement used to define yield.
When a batch shows a position-dependent resistance pattern, the useful question is not simply whether the furnace meets its advertised uniformity specification. It is whether wafers experienced the required temperature history during the relevant process steps, under the actual load, gas flow, ramp, and soak conditions. That distinction guides both troubleshooting and equipment evaluation.
From temperature variation to yield loss
Diffusion is temperature-sensitive: dopant movement depends on temperature as well as time and material conditions. A hotter region generally promotes faster diffusion, while a cooler region can leave a shallower or otherwise different profile. The effect is not necessarily proportional to the temperature difference; diffusion coefficients commonly follow an Arrhenius relationship, so sensitivity must be assessed at the process temperature and for the dopant and material involved.
The electrical result depends on the diffusion sequence. In a predeposition step, temperature can affect dopant incorporation as well as redistribution. During a subsequent drive-in, it can change how deeply an existing dopant population moves. Surface concentration limits, ambient chemistry, oxidation, and the initial dopant distribution can also influence the final profile. Temperature is therefore a plausible cause of variation, not a complete explanation by itself.
A shifted profile may appear as a change in sheet resistance, junction depth, leakage, or other device parameters. A process can lose yield in two ways: individual die can fall outside electrical limits, or an entire wafer or batch can fail a process-control criterion. Conversely, a measurable temperature difference does not automatically mean yield loss. The relevant test is whether it causes a change large enough to consume the available process margin.
Average performance can hide the pattern
A batch average may look acceptable while wafers near one end of the boat consistently differ from those near the center. Similarly, an acceptable wafer-average sheet resistance can conceal an edge-to-center gradient. Evaluators should retain the spatial information behind summary values: wafer position in the load, measurement locations on each wafer, and the relationship of each result to its specification limits.
Attribution also matters. A resistance map is an electrical observation, not a direct temperature map. Dopant source delivery, wafer orientation, gas flow, prior processing, and measurement error can create or reinforce similar patterns. A thermal diagnosis becomes stronger when the electrical pattern tracks an independently measured thermal pattern and responds predictably to a controlled change.
What a uniformity specification actually describes
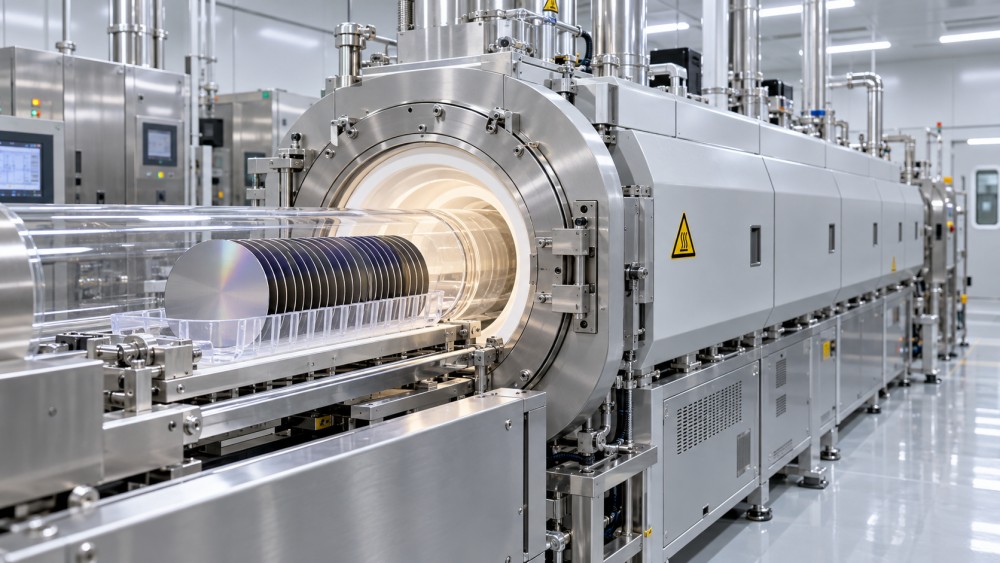
Specifications for Semiconductor Diffusion Furnaces are useful only when their boundaries are clear. A supplier may report uniformity over a defined axial length after stabilization, using a specified sensor arrangement. That result does not automatically describe radial uniformity across a wafer, the temperature during ramping, or the behavior of a loaded boat throughout a production recipe.
Before comparing values, establish whether the number represents a maximum deviation from a setpoint, a range between the highest and lowest readings, or another calculation. A peak-to-peak range and a plus-or-minus deviation are not interchangeable without knowing the reference and calculation. Ask whether the reported value includes measurement uncertainty and whether it applies at each stated operating temperature or only at selected test points.
The location and timing of measurement are equally important. A controller thermocouple can provide reliable feedback for its control loop while still reading a different temperature from the wafer surface. Sensor placement, thermal contact, calibration, and response time affect that relationship. A measurement taken after a long stabilization period may not reveal an earlier excursion during loading or a temperature lag as the furnace ramps.
Separate three questions in an acceptance discussion:
- Control: How closely does each zone follow its setpoint, and how does the system respond to disturbances?
- Thermal field: What spatial and temporal variation is measured within the defined working volume under a specified test load?
- Process result: Do representative wafers meet the electrical and profile requirements across the intended boat positions?
These are related but not equivalent claims. A tool can pass a thermal acceptance test and still require recipe development before it meets a particular product’s process limits.
Where nonuniformity enters a batch
Multi-zone heating is intended to shape the temperature field along the tube, but the resulting field depends on more than the number of zones. Zone tuning, sensor placement, heater condition, insulation, and heat loss at the tube ends can all affect the usable region. A zone setpoint offset may compensate for a repeatable axial gradient, but it should be justified by measured wafer results rather than applied solely to flatten controller readings.
The load changes the thermal problem. Wafer count, spacing, boat material, dummy wafers, and the position of product wafers influence thermal mass and heat transfer. An empty-tube measurement cannot establish the behavior of a full production load. Partial loads may behave differently again, so a qualification based on one configuration should not be assumed to cover every loading pattern.
Gas flow and ambient composition also matter. They can alter heat transfer and, independently, the chemistry responsible for dopant delivery or oxidation. A change in flow that improves one measurement should be checked against the complete process result. Loading and unloading practices, boat insertion timing, and door or end-seal conditions can introduce repeatable temperature transients even when the stable soak looks uniform.
Finally, the wafers accumulate a thermal history rather than experiencing only a nominal soak temperature. Ramp-up, stabilization, process exposure, and cool-down can all contribute to dopant redistribution. For a recipe with significant thermal exposure outside the nominal soak, comparing only the steady-state uniformity can miss an important part of the dose of heat received by different positions.
Diagnosing a position-dependent result
Begin with the failure pattern and preserve its context. Record the recipe revision, furnace and tube, maintenance state, wafer and boat positions, load size, gas settings, and measurement map. Compare affected runs with suitable reference runs using the same product or monitor structure and comparable prior processing. A difference between batches with different upstream histories is not sufficient evidence of a furnace problem.
- Confirm the measurement. Check tool calibration, sampling locations, repeatability, and whether the resistance or junction-depth method is appropriate for the profile. Re-measure selected locations where the procedure permits.
- Separate axial from within-wafer effects. Plot results by boat position and inspect wafer maps. An axial trend suggests a different investigation from a repeatable edge pattern, although both can occur together.
- Review the complete temperature record. Look at zone traces, alarms, ramp timing, stabilization, and deviations from the approved recipe. Controller traces can identify a control event but cannot alone establish wafer temperature.
- Check the physical configuration. Verify sensor condition and calibration, boat and tube condition, load placement, and any recent maintenance or change in gas delivery. Follow site procedures before inspecting hot or hazardous equipment.
- Test one hypothesis at a time. Use an approved monitor run or designed experiment to change a defined factor, such as load configuration or a permitted zone setting. Compare both thermal observations and process measurements against an unchanged reference.
Rotating wafer placement within the boat can help distinguish a position effect from a wafer or upstream effect, provided traceability is maintained and the experiment does not violate the qualified process. For a within-wafer pattern, controlled changes in orientation may help investigate whether the pattern follows the wafer or the furnace environment. Neither test isolates temperature on its own; it narrows the possibilities for the next measurement.
Do not immediately widen process limits to accommodate a shifted distribution. First establish whether the measurement reflects a real profile change, whether the affected population is stable, and whether downstream electrical performance remains within the product’s qualified requirements. A change that improves sheet resistance alone may not preserve junction depth or leakage performance.
Building a meaningful furnace comparison
For equipment evaluation, define the intended operating envelope before requesting a uniformity guarantee: wafer diameter, boat configuration, permitted load range, process temperatures, ramp profile, ambient, and the region in which product wafers will be placed. Include the required process measurements and sampling plan. Otherwise, competing specifications may describe different test conditions rather than different production capability.
Ask suppliers to document the temperature measurement method, sensor calibration and uncertainty, sensor locations, stabilization criteria, and calculation of uniformity. Establish how temperature will be checked across the usable tube length and, where the process requires it, across representative wafer locations. Instrumented wafers or a qualified profiling arrangement may provide more relevant evidence than control sensors alone, but their placement and thermal behavior must also be understood.
A practical acceptance plan separates equipment checks from process qualification. The first can verify agreed control, alarms, repeatability, and thermal measurements under defined conditions. The second uses representative recipes and monitor or product wafers to assess within-wafer and wafer-to-wafer results. Include full and partial loads if both are intended for production, and specify which boat positions count toward acceptance. The plan should state the sample size, measurement locations, calculation method, limits, and treatment of failed or invalid runs before testing starts.
Repeatability deserves separate attention from a single successful run. The relevant evidence is whether the distribution remains controlled over repeated runs and after defined interventions, such as sensor replacement or tube maintenance. Long-term production performance cannot be inferred from a short acceptance test; it requires ongoing control data under the actual product mix and maintenance schedule.
Translating uniformity into a yield decision
Use process data to connect a thermal difference to the electrical parameter that limits yield. Where sufficient data exist, estimate the relationship between temperature or thermal history and the measured response over the approved operating range. Then compare the observed variation with the distance to specification limits, including measurement uncertainty and other sources of process variation. A sensitivity measured for one recipe should not be transferred automatically to another dopant, temperature, or load.
Keep the yield denominator explicit. Die yield, wafer acceptance, and batch release rate answer different questions, and a change in one cannot be assumed to represent the others. A credible assessment identifies the product or monitor, process step, period, number of observations, and rule used to classify failures. When evidence is limited to a thermal profile or a small qualification sample, report that limitation rather than presenting it as sustained production yield.
The decision point is whether the furnace can maintain the required process distribution with adequate margin in the intended operating envelope. If a proposed adjustment achieves this only for one tightly controlled load, that restriction belongs in the operating procedure and capacity assumptions. If the causal link remains uncertain, retain the position-resolved data and continue targeted testing before attributing the loss—or the improvement—to temperature uniformity.
Questions about market trends? Contact Market Scope Live for deeper business insights.
We respect your privacy. Your information is strictly confidential.
We respect your privacy. Your information is strictly confidential.
Related News
 Yield ImprovementWhen can photomask defect inspection miss printable defects?Photomask defect inspection can miss printable defects. Discover key causes, review triggers, and practical ways to strengthen mask quality and wafer yield.MORE+
 Yield ImprovementWhat causes solder joint failure in ball grid array packages?Ball Grid Array Packages can fail due to thermal cycling, board flex, and hidden assembly defects. Discover how to investigate failures and improve reliability.MORE+
 Yield ImprovementWhy Is Wafer Chipping Increasing During Dicing?Why is wafer chipping increasing during dicing? Explore blade, cooling, mounting and process factors, and discover practical steps to protect yield.MORE+
 Yield ImprovementWhat affects photoresist coating uniformity across a wafer?Photoresist Coaters and Developers: Discover what affects wafer coating uniformity and how to troubleshoot thickness variation for a more stable lithography process.MORE+
 Yield ImprovementHow temperature uniformity affects diffusion furnace yieldSemiconductor Diffusion Furnaces depend on temperature uniformity for consistent yields. Explore how to diagnose variations and evaluate furnace performance.MORE+
 Yield ImprovementWhat causes poor contact in semiconductor probe stations?Semiconductor Probe Stations can suffer poor contact due to dirty tips, misalignment, or electrical faults. Discover practical ways to isolate and resolve the cause.MORE+