When can photomask defect inspection miss printable defects?
Author
Date Published
Reading Time
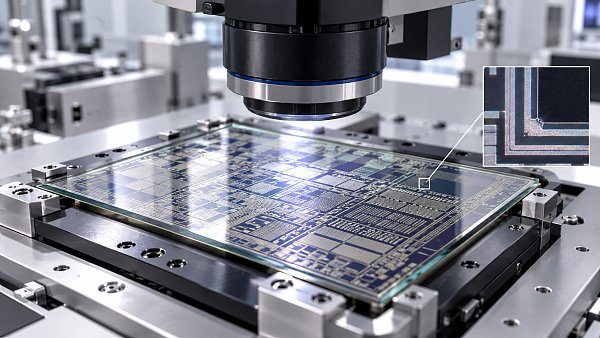
Photomask defect inspection can miss printable defects when inspection sensitivity, imaging conditions, or defect classification do not adequately reflect the lithography process.
Subtle phase variations, low-contrast features, and defects near complex patterns may escape detection or be judged noncritical despite their potential impact on yield.
For quality control and safety managers, the key question is not whether a mask passed inspection, but whether the inspection covered relevant defect types and process conditions.
A pass result is evidence against detected defects within a defined capability. It is not proof that every feature will print correctly across the wafer process window.
Where Can Inspection Miss a Defect That Prints?
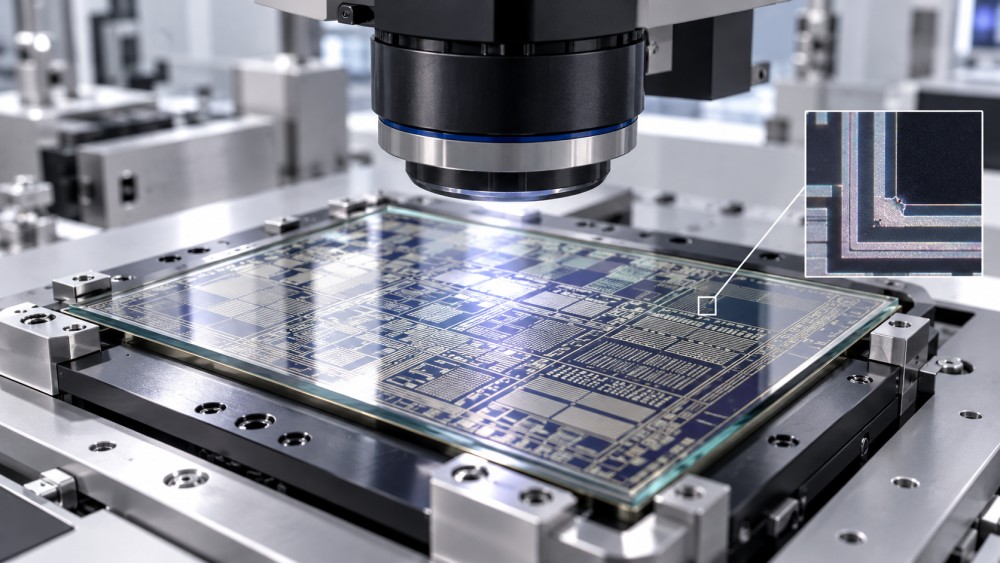
Misses generally occur at three points: the inspection system does not detect an anomaly, the anomaly is classified incorrectly, or its wafer impact is underestimated.
These are different failure modes. Improving image sensitivity may help the first, but it will not necessarily correct an inaccurate disposition rule or incomplete process model.
A printable defect is a mask anomaly that causes an unacceptable wafer pattern under specified exposure and processing conditions. Its impact depends on the design and process.
For example, a small change near a narrow line may alter a critical dimension, while a larger anomaly elsewhere may have no meaningful electrical consequence.
Printability is therefore not an intrinsic yes-or-no label based on mask size alone. It must be evaluated against the intended pattern, process conditions, and acceptance criteria.
Quality teams should also distinguish defects originating on the mask from wafer defects caused by resist, exposure, contamination, etch, or other process steps.
When Is the Inspection Image Different From the Wafer Image?
Mask inspection tools and production scanners may use different wavelengths, illumination geometries, optics, and image processing. Consequently, they may respond differently to the same feature.
An inspection tool can have excellent sensitivity to a particular contrast change and still miss a defect whose effect emerges primarily under the production exposure conditions.
Differences matter especially near the limits of resolution, where small changes in illumination, focus, or pattern context can affect the wafer image and defect ranking.
Inspection recipes should therefore be qualified for the relevant mask technology and layer, rather than assumed equivalent because they use the same equipment platform.
Actinic inspection uses the exposure wavelength relevant to a lithography process, potentially improving representation of certain optical effects. It does not eliminate every detection or classification limitation.
For extreme ultraviolet masks, non-actinic inspection may not reproduce all interactions involving the absorber, multilayer stack, and exposure conditions. Additional review may be necessary for specific risks.
Neither actinic capability nor a vendor specification alone establishes production coverage. Ask which defect types, pattern environments, and operating settings were included in the demonstration.
Which Defects Are Most Likely to Be Underestimated?
Phase and Low-Contrast Defects
A defect can change the phase of reflected or transmitted light without producing an obvious intensity difference in the inspection image. Its wafer effect may still be significant.
On EUV masks, multilayer defects can modify the reflected wavefront. Their visibility and printability depend on their shape, location, absorber pattern, and exposure conditions.
On phase-shift masks, unintended phase or transmission changes can affect image formation even when the mask feature appears close to its intended geometry.
Low-contrast contamination, thin residues, or subtle material variations may also fall below a recipe’s detection threshold. Their risk depends on optical properties and local pattern context.
Defects Near Complex Patterns
Dense patterns, line ends, contacts, and assist features can make small anomalies difficult to separate from intended geometry. Detection performance may vary across these environments.
Optical proximity correction deliberately modifies mask shapes to improve wafer printing. A review process must understand those shapes before treating an apparent irregularity as harmless.
A defect on a subresolution assist feature may not print as a separate feature, yet it can change nearby imaging enough to affect the main pattern.
Similarly, a small bridge, intrusion, or edge displacement may matter more near a narrow process margin than a larger defect in a less sensitive region.
Contamination and Changes After Inspection
A mask can pass inspection and acquire contamination during storage, transport, handling, or use. Inspection timing is therefore as important as the original inspection result.
Pellicles can reduce the likelihood that some particles on their surface are sharply imaged on the wafer, but protection is not absolute or universal.
Pellicle defects, contamination beneath a pellicle, and damage during handling may require distinct detection and response methods appropriate to the mask and exposure system.
Cleaning or repair can also change the risk profile. A previously accepted mask may require reinspection and targeted review after an intervention or suspected event.
How Can Classification Turn a Detected Anomaly Into a Miss?
Detection produces candidates, not final risk decisions. Automatic classification, nuisance filtering, and disposition rules determine which candidates receive attention and which are cleared.
A candidate may be dismissed because its measured size is below a threshold, although its position or optical effect makes it important to the wafer process.
Conversely, an aggressive detection recipe can generate many nuisance signals. High review volume may increase cycle time and make genuinely important candidates harder to prioritize.
Classification performance should be assessed using representative, independently verified examples, including difficult cases. Overall accuracy alone can hide weak performance on rare critical defects.
Track false negatives and false positives separately where ground truth is available. Specify the defect population, pattern types, sample size, and method used to establish truth.
When classification software, reference data, or thresholds change, compare decisions against a controlled baseline and investigate any newly suppressed high-risk candidates before production release.
When Should a Passed Mask Receive Additional Review?
Additional review is most valuable when potential wafer impact is high and the available inspection evidence does not adequately cover the relevant failure mechanism.
Common triggers include new mask materials, a changed exposure recipe, repeated wafer signatures, uncertain repair outcomes, or critical patterns close to their process limits.
A mask may also warrant review after unexplained particle excursions, a pellicle event, abnormal handling, or a change in inspection tool, recipe, or classification software.
Use a documented escalation matrix that identifies the trigger, responsible decision maker, required evidence, and conditions for release, restriction, repair, or quarantine.
Review can include higher-resolution imaging, alternative inspection conditions, defect simulation, aerial image measurement, or wafer exposure. Select the method for the suspected failure mechanism.
Defect review images can clarify geometry and location, but they do not automatically establish printability. The optical and process response may still require separate evaluation.
Aerial image measurements can provide relevant optical evidence for selected conditions, but their relationship to resist and downstream process outcomes must be understood.
Wafer verification can provide direct process evidence, especially for disputed candidates or new recipes. Its value depends on sampling, measurement sensitivity, and exposure conditions.
A clean wafer sample does not prove universal coverage. Rare defects, limited die sampling, and untested focus or dose conditions can leave important uncertainty.
How Should Teams Verify Printability Across the Process Window?
Start with the intended layer, design context, scanner configuration, resist stack, and acceptance criterion. Define whether the concern is a critical dimension, bridge, open, or another outcome.
Use available defect coordinates and mask orientation to connect a candidate with the corresponding wafer location. Confirm alignment and mapping before drawing conclusions from a wafer signature.
Where practical, assess relevant focus and dose conditions rather than relying only on nominal exposure. Some marginal defects appear only near an authorized process-window boundary.
Include downstream process effects when they influence acceptance. A small lithographic variation may become more consequential after etch, while another may not survive processing.
Simulation can help prioritize candidates and explore process conditions, but its conclusions depend on calibrated optical models, defect characterization, and assumptions about the process stack.
Compare model predictions with measured outcomes for representative defects. Revisit the model when materials, scanner settings, mask construction, or downstream processing change.
Document the decision as conditional: identify the tested conditions, measurement limits, acceptance rule, and remaining uncertainty. Avoid describing an untested condition as verified.
What Should a Photomask Inspection Qualification Include?
A useful qualification demonstrates performance on the actual risk landscape, not just a headline minimum detectable defect size supplied under unspecified conditions.
Define representative mask layers, pattern densities, feature orientations, materials, and defect classes. Include both naturally occurring defects and suitable engineered examples where available.
Engineered defects support controlled comparisons, but they may not reproduce the geometry, chemistry, or optical response of naturally occurring contamination and manufacturing defects.
Evaluate detection and disposition together: a candidate found by the tool but consistently filtered out before review still represents an operational coverage gap.
Record inspection settings, tool configuration, reference method, review criteria, and test population. A detection result without these conditions is difficult to compare or reproduce.
Where the reference is another mask image or design data, assess how reference errors, repeated features, and intentional design differences affect candidate identification.
For each critical defect class, establish a measurable coverage objective and an escalation path when qualification evidence is insufficient. Avoid importing thresholds from unrelated layers.
Requalify after significant changes to masks, inspection recipes, software, repair methods, or lithography conditions. Define in advance which changes require partial or full reassessment.
How Can Quality and Safety Managers Control the Risk?
Quality management should connect mask release to wafer consequences, while safety management should ensure that containment, handling, and any intervention follow site-approved procedures.
Assign ownership for mask acceptance, suspected defect escalation, repair authorization, wafer correlation, and final release. Unclear ownership can turn a detectable concern into delayed action.
Maintain traceability from mask identification and revision through inspection recipe, candidate disposition, cleaning or repair history, exposure lots, and relevant wafer measurements.
When a suspected printable defect is found, contain affected masks and potentially exposed lots according to site procedures while the scope and cause are assessed.
Mask handling, cleaning, and repair can introduce separate equipment, chemical, and contamination hazards. Use qualified personnel, approved controls, and applicable facility safety requirements.
Do not treat inspection acceptance as authorization to bypass those controls. Process quality decisions and personnel safety decisions are related but require separate evidence.
For recurring problems, monitor trends by layer, defect class, supplier, inspection recipe, and mask lifecycle stage. Investigate changes in both confirmed defects and nuisance rates.
Useful indicators include confirmed escape events, review backlog, time to disposition, and repeat defects. Interpret rates with defined populations and time periods, not isolated totals.
What Should Buyers Ask an Inspection Supplier?
Request evidence for the specific mask technology and defect mechanisms of concern, including pattern context, inspection settings, reference method, and independently verified outcomes where available.
Ask how the supplier measures detection sensitivity and false calls, and whether reported results include candidate classification and the final disposition workflow.
Compare throughput at the proposed sensitivity and production recipe, including review workload and expected maintenance. A maximum throughput figure may not represent sustained operating performance.
Clarify integration with defect review, data retention, mask tracking, software updates, service support, and acceptance testing. Identify who will supply representative masks and establish ground truth.
Finally, agree on limits: which defect classes remain weakly covered, what complementary methods are needed, and how recipe changes will be validated after installation.
Conclusion: Treat Inspection as One Layer of Evidence
Photomask defect inspection can miss printable defects when detection, imaging, classification, or inspection timing fails to match the relevant mask and wafer process conditions.
The strongest release decision combines qualified inspection, risk-based review, controlled handling, traceable records, and wafer-level evidence where uncertainty or potential impact justifies it.
For managers, the practical test is clear: know what the inspection can detect, what it can miss, and who acts when the evidence is incomplete.
Questions about market trends? Contact Market Scope Live for deeper business insights.
We respect your privacy. Your information is strictly confidential.
We respect your privacy. Your information is strictly confidential.
Related News
 Yield ImprovementWhen can photomask defect inspection miss printable defects?Photomask defect inspection can miss printable defects. Discover key causes, review triggers, and practical ways to strengthen mask quality and wafer yield.MORE+
 Yield ImprovementWhat causes solder joint failure in ball grid array packages?Ball Grid Array Packages can fail due to thermal cycling, board flex, and hidden assembly defects. Discover how to investigate failures and improve reliability.MORE+
 Yield ImprovementWhy Is Wafer Chipping Increasing During Dicing?Why is wafer chipping increasing during dicing? Explore blade, cooling, mounting and process factors, and discover practical steps to protect yield.MORE+
 Yield ImprovementWhat affects photoresist coating uniformity across a wafer?Photoresist Coaters and Developers: Discover what affects wafer coating uniformity and how to troubleshoot thickness variation for a more stable lithography process.MORE+
 Yield ImprovementHow temperature uniformity affects diffusion furnace yieldSemiconductor Diffusion Furnaces depend on temperature uniformity for consistent yields. Explore how to diagnose variations and evaluate furnace performance.MORE+
 Yield ImprovementWhat causes poor contact in semiconductor probe stations?Semiconductor Probe Stations can suffer poor contact due to dirty tips, misalignment, or electrical faults. Discover practical ways to isolate and resolve the cause.MORE+