When do semiconductor packaging substrates need finer line widths?
Author
Date Published
Reading Time
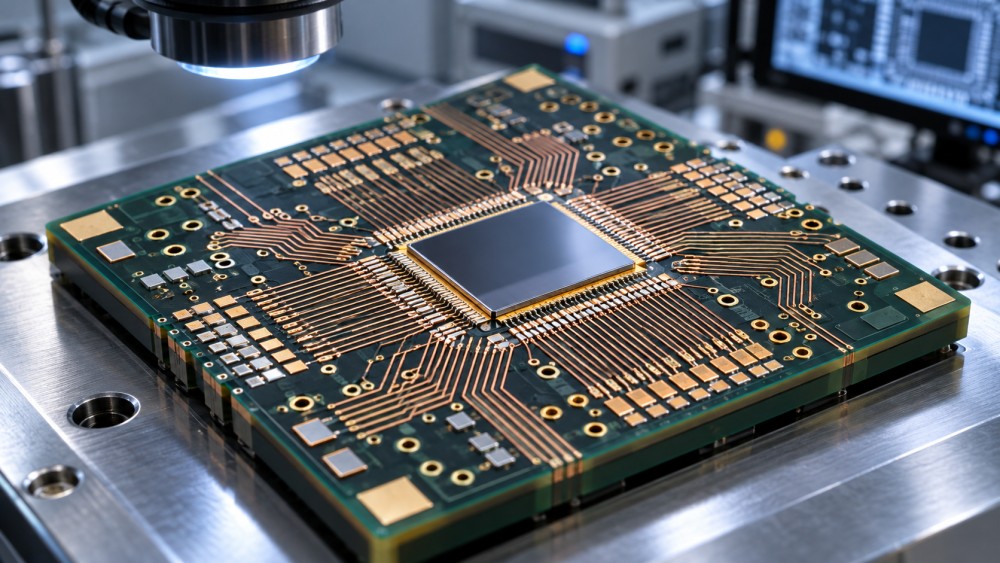
Semiconductor Packaging Substrates need finer line widths when the required connections cannot be routed through the available area using a manufacturable coarser geometry. The trigger may be a dense die interface, a narrow escape-routing channel, a high-I/O processor, or a chiplet arrangement with limited space between connections. A finer process is justified when it resolves a demonstrated routing constraint without creating unacceptable electrical, reliability, yield, or cost penalties.
The immediate decision is not whether the smallest advertised line is available. It is whether a particular layer and region need narrower lines and spaces, and whether the complete package can be built and qualified at the intended volume. A design that routes on screen but cannot meet impedance, current, inspection, or production requirements has not yet solved the problem.
Start with the routing bottleneck, not the minimum feature
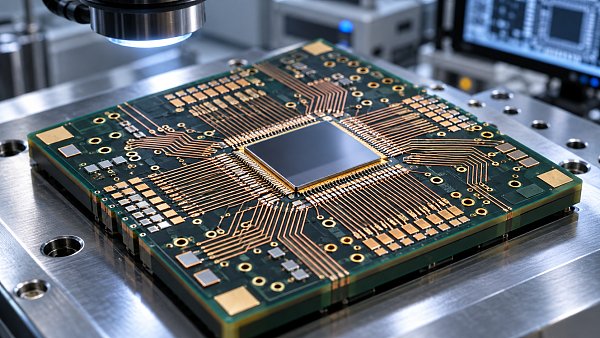
A substrate connects die-side features to a larger package footprint through patterned conductors, dielectric layers, and vias. As connection density rises, traces must escape from closely spaced pads and travel through restricted areas before reaching their destinations. The limiting point is often local: a channel between via arrays, the edge of a die footprint, or a transition between dense and less dense regions.
Before requesting a finer process, identify the nets that cannot be routed and the rule that blocks them. A routing report should distinguish congestion caused by trace width and spacing from congestion caused by via diameter, capture pads, keep-out regions, layer transitions, or an unfavorable pin assignment. Narrower traces alone may not help if via structures still occupy the available channel.
Line width and space are normally discussed together. Width is the conductor dimension; space is the separation between adjacent conductors. Both influence how many routes can fit, but neither should be treated as the entire design rule. Ask the supplier whether its quoted dimensions apply across all relevant layers and pattern lengths, and whether they are nominal targets, minimum design rules, or measured production capabilities.
Signals that a finer geometry may be necessary
Die escape consumes the available channels
A dense die-side connection array can leave too little room to route the required signals outward while respecting conductor spacing, via clearance, and reference-plane rules. Examine the most constrained rows and columns rather than relying only on total I/O count. Two packages with the same number of connections can have different escape difficulty because their pad arrangements, power connections, and keep-out zones differ.
Finer lines and spaces can create additional paths in those channels. The decision is stronger when a design-rule-compliant routing study shows that the existing geometry fails even after reasonable pin reassignment and layer allocation. It is weaker when the apparent blockage results from a provisional pin map that the die and system teams can still change.
Chiplet connections crowd a shared region
Multi-die packages may place a large number of short interconnects between neighboring devices. The available routing region can be restricted by die placement, power delivery, thermal structures, and assembly tolerances. In such a layout, finer substrate routing may help, but it is not automatically the right integration layer.
First establish where the dense connections must be made. Depending on the required pitch and electrical behavior, the practical options may include a finer organic substrate, a redistribution layer, an interposer, or another local interconnect structure. Each introduces its own fabrication, assembly, test, and supply requirements. A substrate supplier’s minimum line width should not be compared directly with another technology’s headline feature size without comparing the complete stack and connection rules.
Adding layers no longer solves the whole problem
More routing layers can relieve congestion, but they also introduce additional transitions, stack thickness, processing steps, and potential alignment or reliability concerns. A layer-count increase may be acceptable when congestion is distributed across the package. It may be much less effective when the true constraint is escape from a small die-side region and the vias needed to reach those layers consume the same scarce area.
Compare feasible stackups rather than assuming either finer features or more layers will win. The relevant result is a complete routed design with viable via access, reference planes, power delivery, and manufacturing rules—not the number of signal tracks in an isolated cross-section.
Check what narrower conductors do to the electrical design
Routing capacity is only one side of the decision. Reducing trace width can increase conductor resistance for a given material, thickness, and length. That may affect voltage drop and loss, especially where long routes or current-carrying conductors are involved. Copper thickness and the actual conductor cross-section matter; a nominal width by itself is not enough to calculate the result.
Signal integrity also needs a stackup-specific review. Trace geometry, dielectric properties, nearby reference planes, spacing, and transitions all influence impedance, coupling, and loss. A narrower trace is not inherently better for a high-speed signal. Maintaining a target impedance may require changes to dielectric thickness or trace geometry, and those changes can affect manufacturability elsewhere in the stack.
Power and ground should be assessed separately from signal routing. Fine signal lines may free space locally, but power delivery still depends on plane area, via capacity, current paths, decoupling placement, and acceptable noise and voltage drop. Do not count a routing solution as complete if it removes the reference continuity or power structure needed by the electrical design.
Use extraction and simulation with the supplier’s proposed stackup and realistic geometry tolerances. Then identify the features that are sensitive to variation: minimum-width segments, long parallel runs, dense via fields, and transitions between layers. Simulation is a screening tool; test structures and package-level measurements are needed to confirm the assumptions used for a qualified design.
Compare the alternatives before changing the process node
These choices can be combined. A package may use fine routing only on selected layers while retaining coarser features elsewhere. That approach can preserve capacity where it is needed, but the supplier must confirm the allowable transitions, registration requirements, and stackup. A mixed-rule design is not automatically cheaper if it introduces process complexity or reduces yield.
Turn a supplier capability claim into a usable design rule
Fine-feature capability can mean a laboratory demonstration, a process under qualification, or repeatable production on a particular substrate construction. Those are different levels of readiness. Ask for the scope behind the claim: substrate material, layer position, panel or substrate size, copper thickness, line and space combination, via structures, and the design-rule manual applicable to the proposed build.
Several details deserve explicit clarification before a layout is frozen:
- Geometry and tolerances: Determine how widths, spaces, registration, and copper thickness are specified and measured. Confirm whether the minimum applies to long traces, dense arrays, and the actual layer under consideration.
- Via compatibility: Obtain rules for via size, capture pads, clearances, stacking, and transitions. A fine trace pitch has limited value if compatible via structures cannot support the escape pattern.
- Inspection and defect controls: Ask how opens, shorts, dimensional variation, and relevant layer-to-layer alignment are detected, and what test coverage is available for the proposed structures.
- Reliability evidence: Request results applicable to the intended materials, stackup, assembly process, and service conditions. Check the test methods and sample boundaries rather than treating an unrelated qualification as transferable.
- Capacity and change control: Establish whether the process is available for development builds or sustained supply, along with lead times, material dependencies, and how process changes would be communicated and requalified.
A supplier may offer a design-rule limit that is technically achievable but leaves little margin for a complex production layout. Review not only the smallest feature, but also the density and length over which it is used. The yield effect depends on defect mechanisms, pattern area, inspection, repair or disposition rules, and the package construction; it cannot be inferred from line width alone.
Make the decision with a comparable build plan
Prepare two or more candidate implementations using the same functional requirements: connection count, package outline, electrical limits, thermal constraints, and expected volume. For each, record the routing completion, layer count, via structures, stackup, predicted electrical performance, and unresolved design-rule exceptions. Include at least one layout using the current geometry if it is technically plausible.
Next, request supplier feedback and quotations against those candidate designs, not against a feature-size headline. Define what the quotation includes: engineering work, masks or tooling where applicable, prototype quantities, electrical test, inspection, qualification support, and production assumptions. A lower unit quote on one configuration may not cover the same test scope or yield responsibility as another.
Use a representative test vehicle or early build to examine the highest-risk structures before committing to a full qualification plan. Dense escape patterns, long minimum-width runs, via transitions, and critical high-speed or power structures are more informative than a coupon containing only isolated fine lines. Agree in advance on measurements, acceptance criteria, sample scope, and how failures will be analyzed. A successful prototype supports the next decision; it does not by itself establish sustained production yield.
Choose finer line widths when the routing and electrical studies show that alternatives cannot meet the package requirements at acceptable risk, and when a supplier can support the required geometry in the actual construction. If the only evidence is that a smaller feature exists, keep the design choice open until the complete stackup, qualification path, and supply conditions are clear.
Questions about market trends? Contact Market Scope Live for deeper business insights.
We respect your privacy. Your information is strictly confidential.
We respect your privacy. Your information is strictly confidential.
Related News
 Advanced PackagingHow accurate do die bonders need to be for flip-chip assembly?Die Bonders for flip-chip assembly must meet post-bond alignment targets. Explore accuracy budgets, process factors and practical tips for choosing the right machine.MORE+
 Advanced PackagingWhen does system-in-package make sense for compact devices?System-in-Package can unlock space and performance in compact devices. Explore the thermal, cost, yield, and supply trade-offs before choosing SiP.MORE+
 Advanced PackagingHow to choose wire bonding equipment for fine-pitch devicesChoose Wire Bonding Equipment for fine-pitch devices with confidence. Compare placement accuracy, bond quality, throughput, supplier trials and ownership costs.MORE+
 Advanced PackagingWhy does ABF substrate warpage matter during chip assembly?ABF Substrates can warp during chip assembly, putting yield and reliability at risk. Discover how to measure deformation and control defects.MORE+
 Advanced PackagingHow Much Floor Space Does a Wire Bonding Machine Need?How much floor space does a wire bonding machine need? Explore footprint, access, utilities, and layout planning to make a confident equipment decision.MORE+
 Advanced PackagingCan a Die Bonder Handle Warped Wafers?How do I check whether a die bonder can handle warped wafers? Compare measurement methods, review process limits, and verify performance with representative wafers.MORE+
 Advanced PackagingWhen do semiconductor packaging substrates need finer line widths?When do Semiconductor Packaging Substrates need finer lines? Explore routing bottlenecks, electrical trade-offs, and supplier checks to make a confident design decision.MORE+
 Advanced PackagingHow underfill materials reduce thermal fatigue in flip-chip packagesDiscover how Semiconductor Underfill Materials reduce flip-chip thermal fatigue, and learn what to consider when selecting and qualifying a formulation.MORE+